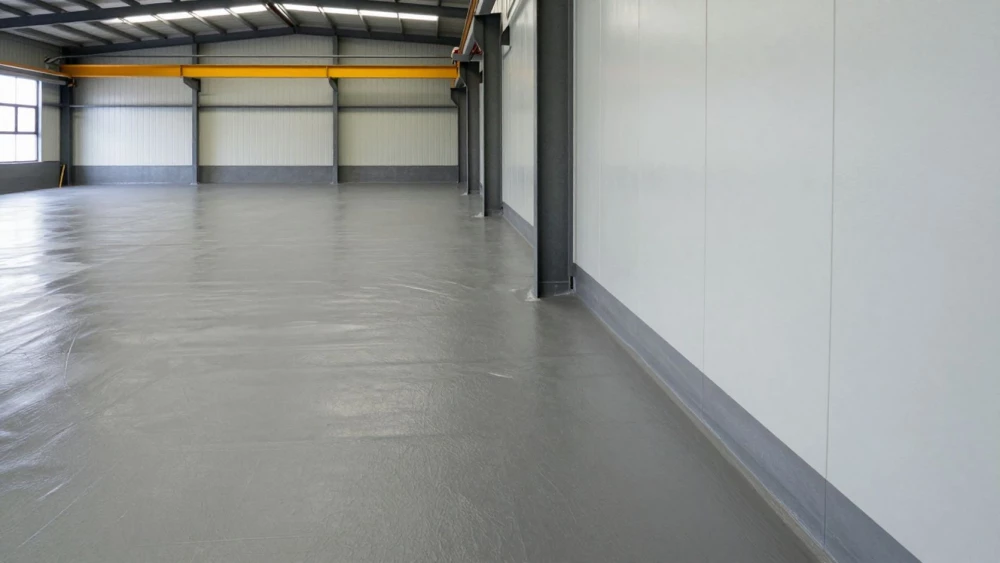
Chemical Resistant Flooring
Get in TouchAt Factory Flooring, we specialise in providing robust chemical resistant flooring solutions. Our flooring is designed to protect against the harsh impact of chemicals, ensuring long-lasting durability and safety.
We use advanced materials like epoxy and polyurethane to offer floors that withstand corrosive substances, heavy machinery, and high foot traffic typically found in industrial environments. Whether it's a laboratory, manufacturing plant, or warehouse, our tailored flooring systems meet all specific needs.
Covering and the surrounding postcode area, we provide expert advice and precise installations to ensure complete customer satisfaction.
How Much Does Chemical Resistant Flooring Cost?
Chemical resistant flooring costs around £70 to £100 per m². Several factors influence this price, including the type of material used, area size, and the existing condition of the substrate.
Epoxy flooring tends to be more cost-effective, while polyurethane can offer enhanced chemical resistance at a higher price point. The choice between materials may also depend on compliance with industry standards such as ISO 2815 and ASTM D4060, which ensure thickness and abrasion resistance.
The complexity of the installation also impacts cost, as intricate designs or uneven surfaces require more time and resources. The need for additional preparatory work, such as substrate smoothing or applying moisture barriers, can further influence expenses.
Typically, the entire process, from preparation to final installation, can take between two to five days, depending on project size and complexity. Contact us today to get a tailored quote for your flooring project.
Book Chemical Resistant Flooring Today
What Types of Chemical Resistant Flooring Are Available?
We offer a variety of chemical resistant flooring options to suit different industrial needs and environments:
Epoxy Flooring: Known for its durability and ease of maintenance, epoxy flooring is ideal for environments exposed to medium chemical exposure. It meets the standards for slip resistance and can withstand heavy machinery. Typically installed within two days, it's suitable for warehouses and manufacturing units.
Polyurethane Flooring: This flooring offers higher chemical resistance and elasticity, making it suitable for areas subject to thermal shock and dynamic loads. Polyurethane can tolerate UV exposure, making it great for outdoor facilities or areas with fluctuating temperatures.
Vinyl Ester Flooring: Excellent for highly corrosive environments such as chemical processing plants, vinyl ester flooring provides robust protection against acids and alkalis. It creates a surface that complies with hygiene standards, often used in pharmaceutical and food production sectors.
MMA (Methyl Methacrylate) Flooring: With its fast-curing properties, MMA flooring minimises downtime, curing in as little as one hour. Its versatility in colour and texture makes it appealing for areas with aesthetic requirements, such as retail spaces.
Each type varies in terms of installation time, cost, and specific benefits. We can help you choose the right fit for your facility based on these specifications.
How Long Does Chemical Resistant Flooring Last?
Our chemical resistant flooring typically lasts between 10 to 15 years, depending on the level of chemical exposure and maintenance. We often use materials such as epoxy and vinyl ester resins, which provide excellent resistance to acids, alkalis, and solvents.
Regular cleaning with industry-approved agents and the application of protective coatings like urethane can extend the lifespan further. The flooring's durability also depends on factors such as thickness, with floors of 3 to 5 mm typically providing better longevity in heavy-duty environments like laboratories and manufacturing plants.
Adhering to standards like ISO 9001 ensures quality in our installation processes. For advice on selecting the appropriate material for your specific environment, reach out to our team for tailored recommendations.
What Are the Benefits of Chemical Resistant Flooring?
Opting for chemical resistant flooring provides several benefits, making it a top choice for industrial spaces. These flooring solutions are specifically designed to meet industry standards, such as ISO 2812-1 for testing chemical resistance to ensure they stand up to rigorous conditions.
Durability: Withstands heavy machinery and constant foot traffic over time, extending the lifespan of the flooring even in demanding environments. Materials like epoxy and polyurethane are commonly used for their robustness.
Chemical Protection: Resistant to corrosive and potentially damaging substances, including acids, alkalis, and solvents. This protection is crucial for industries such as pharmaceuticals and food processing where spills are common.
Safety: Provides a slip-resistant surface, enhancing workplace safety. The use of additives, like aluminium oxide, increases traction, preventing accidents in wet conditions.
Low Maintenance: Easy to clean and maintain, reducing long-term costs. The non-porous surface prevents bacterial growth, making it hygienic and ideal for medical facilities.
These versatile benefits make chemical resistant flooring a practical choice for maintaining functional and safe industrial operations. Contact us to discuss how these benefits can enhance your workspace.
Why Choose Factory Flooring for Chemical Resistant Flooring?
Choosing Factory Flooring ensures you receive expert advice and comprehensive installation of chemical resistant flooring. We specialise in a range of materials such as epoxy resins and polyurethane coatings, which are formulated to withstand harsh chemicals, including acids and alkalis.
Our team is experienced in working with diverse industrial environments, from pharmaceutical plants to food processing facilities, ensuring each installation is tailored to meet specific needs and industry regulations. We employ precise application techniques, such as squeegeeing and roller methods, to achieve uniform coverage and optimal thickness.
Our installations align with safety and quality standards, including EN 13501 for fire resistance and ISO 9001 for quality management. Trust us to provide the right solution for your flooring requirements, offering enhanced resistance to abrasion and impact.
Our projects typically take one to two weeks from preparation to cure, minimising downtime. Reach out today to get started on your project.
Speak to a Chemical Resistant Flooring Expert
Frequently Asked Questions
How do I maintain chemical resistant flooring?
Maintaining chemical resistant flooring involves routine cleaning with non-abrasive tools and mild detergents. Avoid harsh chemicals to preserve the integrity of the floor coating.
Regular inspections help address minor damages to extend lifespan.
Do I need special permits for installing chemical resistant flooring in a commercial setting?
In most cases, no special permits are required for installing chemical resistant flooring. However, it is advisable to check local regulations and consult with professionals to ensure compliance.
Can I install chemical resistant flooring myself?
We recommend professional installation. Our team at Factory Flooring has the expertise to manage the complexities of industrial flooring installation, ensuring a and durable finish.
Get a Free Quote for Chemical Resistant Flooring
Protect your industrial space with our reliable chemical resistant flooring solutions. today to discuss your needs and find the best flooring solution for your facility.