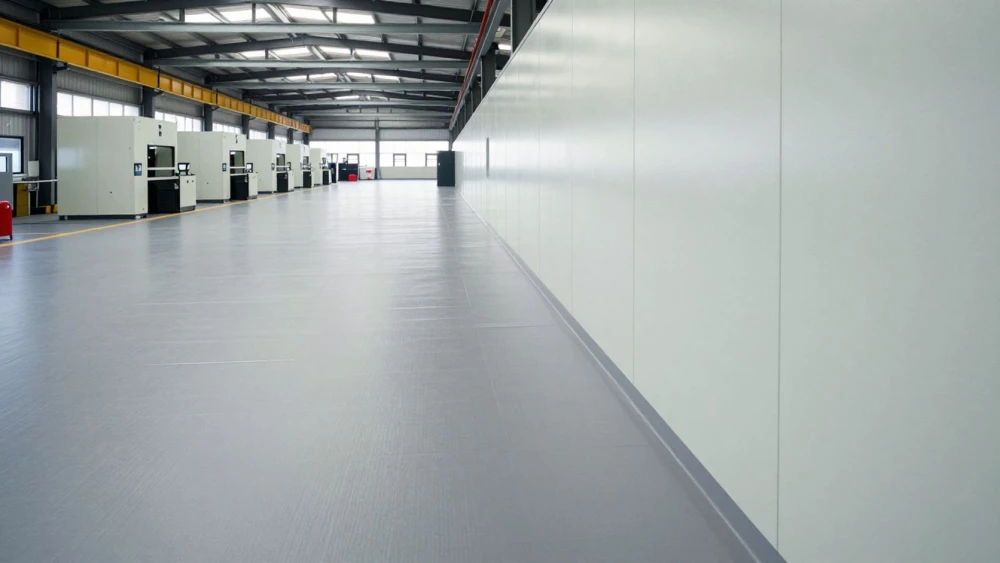
Industrial Floor Coatings
Get in TouchAt Factory Flooring, we provide industrial floor coatings for a range of demanding environments. Our coatings offer durability and resistance against chemicals, impacts and abrasions, making them ideal for factories, warehouses, and commercial settings.
We use materials such as epoxy and polyurethane to ensure long-lasting performance. Our services cover the area, enhancing both safety and functionality in industrial spaces.
Contact us today to discuss your flooring needs.
Book Industrial Floor Coatings Today
How Much Do Industrial Floor Coatings Cost?
Industrial floor coatings typically cost between £25 and £50 per m². The cost varies depending on the type of coating selected, the condition of the existing floor, and any additional preparation work required.
Epoxy coatings are often an economical option, while polyurethane might come at a higher cost due to its superior chemical resistance. Polyurethane is particularly valued in environments with exposure to harsh chemicals, such as factories and laboratories.
The condition of the existing floor can significantly impact costs: repairing cracks or leveling the substrate may add to the overall expense. We assess the floor's moisture content and temperature before proceeding, ensuring proper adhesion and durability.
The installation process typically takes between two and three days, in line with industry standards. For more precise pricing and project timelines, we provide detailed quotes after assessing your specific project requirements.
Let's help transform your flooring solution.
What Types of Industrial Floor Coatings Are Available?
We offer a variety of industrial floor coatings to suit different applications and meet diverse industry requirements:
Epoxy Coatings: Known for their strong adhesion and hard-wearing finish. These are ideal for areas with heavy foot traffic and can be customised in different textures and colours to enhance slip resistance.
Polyurethane Coatings: Flexible yet robust, making them suitable for areas with heavy machinery. They also resist chemical spills and abrasions, conforming to safety standards in manufacturing environments.
Acrylic Coatings: Quick-drying, offering fast turnaround times, which makes them perfect for warehouses or retails spaces needing minimal downtime. They also provide a glossy finish that is aesthetically pleasing.
Polyaspartic Coatings: Resistant to UV light, preventing discolouration. They cure rapidly even in low temperatures and are often used in outdoor and refrigerated settings.
Each type is tailored to specific operational needs, and we can advise on the best choice for your facility to ensure durability and performance.
How Long Does It Take to Apply Industrial Floor Coatings?
Applying industrial floor coatings generally takes two to three days, depending on the surface area and preparation needed. We begin by assessing the condition of your existing floor and addressing issues such as cracks or uneven surfaces, often using diamond grinding for a smooth base.
This ensures optimal adhesion of the coating, which is commonly an epoxy or polyurethane type known for its durability and chemical resistance. The curing time can vary, with most epoxy floors ready for light use after 48 hours.
Polyurethane coatings might need a little longer, typically 72 hours, to fully cure. Factors like ventilation and temperature can affect the drying process: warmer temperatures can accelerate curing, while cold can delay it.
We ensure minimal disruption to your operations by scheduling work during off-peak hours, often completing installations for warehouses or factories over weekends or overnight. For further details, contact us to discuss your specific flooring needs.
What Are the Benefits of Industrial Floor Coatings?
Industrial floor coatings offer numerous advantages for a variety of industrial facilities such as factories, warehouses, and manufacturing plants. They are designed to meet the rigorous demands of environments frequently exposed to wear and tear.
Durability and Longevity: Our epoxy and polyurethane coatings are able to withstand heavy use and harsh conditions, providing long-lasting protection for your floors.
Chemical Resistance: Protect surfaces from spills and corrosive materials, safeguarding floors against damage from chemicals like acids, alkalis, and solvents.
Improved Safety: Reduce slip hazards with non-slip, textured surfaces that comply with safety standards, enhancing overall workplace safety.
Aesthetic Appeal: Enhance the appearance of industrial environments with a range of finishes and colours, contributing to a clean and professional look.
These benefits, combined with our expert application services, make our coatings a smart investment for any industrial facility seeking functional and visually appealing flooring solutions. Contact us to explore options tailored to your specific needs.
How Long Do Industrial Floor Coatings Last?
Industrial floor coatings typically last 5 to 10 years, depending on usage and maintenance practices. Among various options, epoxy floors are popular, offering around eight years of solid performance when well-maintained.
Polyurethane coatings, another choice, are noted for their UV resistance and flexibility, often used in areas exposed to sunlight. Environmental factors, such as chemical exposure and traffic volume, can significantly influence their lifespan.
For instance, in chemical processing plants, floors may experience aggressive chemical interactions that require specialised coatings with high chemical resistance, such as polyaspartic or novolac epoxy.
Regular cleaning, using pH-neutral cleaners, and timely repairs to address scratches or cracks can further extend the durability of these coatings. Employing preventative measures like installing protective pads under heavy machinery can also help preserve the floor.
With proper care, some coatings may exceed the typical lifespan, ensuring uninterrupted performance. Contact us for advice tailored to your specific floor coating needs.
Why Choose Factory Flooring for Industrial Floor Coatings?
Choosing Factory Flooring for industrial floor coatings ensures expertise and quality. Our experienced team uses high-grade epoxy and polyurethane materials and advanced application techniques such as self-levelling and broadcast systems to deliver durable flooring solutions.
We conduct thorough surface preparation techniques, including shot blasting and diamond grinding, to ensure optimal adhesion and longevity. Our coatings are designed to withstand the rigours of heavy machinery, high foot traffic, and chemical exposure, making them suitable for manufacturing facilities, warehouses, and automotive workshops.
We offer personalised advice to match each client’s specific needs and adhere to industry standards such as ISO 9001 for quality management and ISO 45001 for occupational health and safety. Our attention to detail in achieving specific thickness and texture requirements ensures a customised fit for various operational environments.
Get in touch today for a lasting flooring upgrade.
Speak to an Industrial Floor Coatings Expert
Frequently Asked Questions
How do I maintain industrial floor coatings?
Maintaining industrial floor coatings involves regular sweeping and mopping to remove dirt and debris. Spillages should be cleaned promptly using non-abrasive cleaners designed for coated surfaces.
Annual inspections are recommended to address minor damages.
Do I need to close my operations during the coating process?
Depending on the area being coated, it might be necessary to close operations temporarily. However, we strive to minimise disruptions by working at flexible hours and in sections.
Can industrial floor coatings withstand heavy machinery?
Yes, our industrial floor coatings are designed to endure the weight and movement of heavy machinery, particularly the durable options like polyurethane and polyaspartic.
Which areas do you cover for industrial floor coatings?
We cover and the surrounding area, ensuring reliable service wherever your facility is located. Our team can discuss specific locations during consultation.
Are there colour options for industrial floor coatings?
Yes, we provide a variety of colour options to match your aesthetic requirements. Custom colouring can be arranged to align with brand or safety needs.
Get a Free Quote for Industrial Floor Coatings
Interested in enhancing your industrial space with our floor coatings? today and let Factory Flooring bring durability and style to your facility.